In every process plant — refineries, pharmaceutical reactors, power boilers, food sterilizers, water treatment trains — temperature is one of the most critical variables the control system has to trust. A drifting or noisy temperature loop can spoil a batch, trip a unit, or silently waste energy for months before anyone notices. The component that sits between the raw sensor signal and the DCS or PLC, and decides how trustworthy that loop is, is the temperature transmitter.
This guide walks through how modern smart temperature transmitters actually work, why cold junction compensation matters, how to calibrate them correctly (and why “calibration” is not the same as “re-ranging”), and the field installation rules that quietly determine measurement quality on day one.
1. What a Temperature Transmitter Actually Does
An RTD or thermocouple, on its own, produces a very small signal — a few millivolts for a thermocouple, or a tiny resistance change for an RTD. Running that signal long distances directly to a control room over plain cable is a recipe for noise pickup, lead-wire error and drift.
A temperature transmitter is a signal-conditioning device that:
- Reads the sensor — RTD, thermocouple, mV, or resistance input.
- Linearizes the raw signal against the sensor’s standard characteristic curve.
- Compensates for environmental effects — cold-junction temperature for thermocouples, lead resistance for RTDs.
- Converts the result into a robust, standardized output: 4–20 mA, 4–20 mA + HART, FOUNDATION Fieldbus H1, PROFIBUS PA, WirelessHART, or Modbus RTU.
The output side is what makes the transmitter useful. A 4–20 mA loop or fieldbus signal can run hundreds of metres through an industrial environment without losing accuracy — something the raw sensor signal cannot.

2. The Signal Chain Inside a Smart Temperature Transmitter
Modern smart transmitters — for example the Microcyber NCS-TT105, NCS-TT106, and NCS-TT108 series — share a similar internal architecture:
- Input front end – multiplexer and high-resolution ADC capable of reading multiple sensor types: Pt100, Pt1000, Cu50, Cu100 RTDs in 2-, 3-, or 4-wire configuration, plus thermocouples of types B, E, J, K, N, R, S, T.
- Cold-junction sensor – an internal temperature reference at the terminal block, used to compensate thermocouple readings.
- Microprocessor and firmware – applies the sensor characterization curve, performs linearization, runs diagnostics, stores configuration.
- Communication / output stage – generates the 4–20 mA current and modulates HART, or drives the digital fieldbus interface for PA / FF / WirelessHART models.
- Galvanic isolation – separates the sensor input from the output and the power supply. On industrial-grade modules this isolation is rated up to DC 1000 V, protecting the DCS from ground loops and sensor-side faults.
Because all of this runs in firmware rather than in fixed analog circuitry, a smart transmitter can also store calibration history, output secondary variables (such as terminal temperature), perform sensor drift detection, and support dual-sensor features like hot backup or differential-temperature calculation.

3. Cold Junction Compensation — Where Most Thermocouple Errors Come From
A thermocouple does not measure absolute temperature. It measures the difference between the hot junction (in the process) and the cold junction — the terminal block where the TC wire meets copper wire inside the transmitter. If the cold junction sits at 30 °C and you ignore that fact, the reading is off by roughly 30 °C.
A smart temperature transmitter solves this with an internal temperature sensor located right at its terminal block. The firmware reads cold-junction temperature in real time and adds an equivalent millivolt correction to the measured TC voltage.
Quality matters here. On industrial-grade smart transmitters such as the NCS-TT106 series, cold-junction compensation accuracy is specified to within ±0.15 °C (with an external Pt100 measuring the cold junction). Combined with the transmitter’s basic accuracy class (better than 0.1 %) and its temperature drift specification (typically better than ±50 ppm/°C), this is what determines what the loop can actually achieve in the field — not the headline number on the data sheet.
For RTD inputs, the equivalent concern is lead-wire resistance, which is why 3-wire and 4-wire connections exist. A 4-wire RTD cancels lead resistance completely; a 3-wire cancels it only on the assumption that all three leads are identical in length and gauge.

4. Calibration: Sensor Trim vs Output Trim vs Re-ranging
The single most common mistake in temperature loop maintenance is treating “calibration” as adjusting zero and span on a HART communicator. That is re-ranging, not calibration. True calibration requires a traceable physical reference.
A proper smart-transmitter calibration involves up to three distinct operations:
Sensor trim (input trim). The transmitter is fed a known physical input — a precision resistance for an RTD, or a millivolt source / temperature bath for a thermocouple — and the firmware is told what that input actually represents. This corrects the input section against the reference, and is the only part that fixes real measurement error in the sensor input chain.
Output trim (4–20 mA trim). The transmitter is commanded to output exactly 4.000 mA and 20.000 mA, while an accurate reference ammeter measures the actual current. Any offset is trimmed out. This matters when the analog signal is what the control system reads; for purely digital loops (HART-as-primary, FF, or PA) it is generally not required.
Re-ranging. Setting LRV and URV — for example, 0 °C = 4 mA and 200 °C = 20 mA. This is configuration, not calibration, and on its own it does not assure transmitter accuracy.
A clean field procedure for a typical RTD/HART loop looks like this:
- After power-up, let the transmitter stabilize for at least 5–15 minutes before any adjustment.
- Apply the lower reference temperature (e.g., 0 °C) in a dry-block or temperature bath. Wait for full thermal stabilization — at least 15–20 minutes is realistic.
- Compare the transmitter’s PV (read over HART) to the traceable reference. If outside tolerance, perform sensor trim — lower.
- Apply the upper reference (e.g., 100 % of range). Wait for stabilization. Perform sensor trim — upper.
- Verify linearity at an intermediate point — typically 50 % of span.
- If the 4–20 mA is the control signal, perform output trim at 4 mA and 20 mA against a calibrated mA reference.
- Document the as-found and as-left values.
A useful field interval is every 6 to 12 months for general service, and tighter for safety-instrumented or custody-transfer loops. Smart transmitters with low temperature drift hold calibration well between intervals, but the interval should be set by criticality, not by the device data sheet alone.
Important: a HART communicator on its own cannot calibrate a transmitter. It can configure, re-range, and report — but the metrological calibration always requires a separate, accurate reference.
5. Field Installation: Where Loops Quietly Fail
Most “transmitter problems” turn out to be installation problems. The points below are worth checking before blaming the device.
Sensor wiring
- Use the correct number of leads. A 3-wire RTD wired into a 2-wire pattern will read low by the lead resistance.
- For thermocouple extension, use matching TC-grade compensating cable all the way to the transmitter terminals. Copper extension defeats cold junction compensation.
- Tighten the terminals. Loose terminals are a classic source of intermittent drift.
Cable, shielding, grounding
- Run signal cables as shielded twisted pair, physically separated from power cables.
- Ground the shield at one end only — typically the control room side — to avoid ground loops.
- For long runs in noisy environments, a head-mounted smart transmitter is far more robust than running raw RTD / TC signals back to a marshalling cabinet.
Mechanical and environmental
- Install the sensor at sufficient immersion depth — typically 8–10× the thermowell diameter — so the sensing element actually reaches process temperature.
- For field-mounted transmitters, confirm the housing rating against the environment. IP66 / IP67 is standard for outdoor or washdown service.
- In high-temperature applications (process side > 100 °C), keep the transmitter electronics thermally separated from the process. Extension necks, insulating barriers, and remote-mount configurations exist for exactly this reason; excess heat soaking into the transmitter is one of the top causes of premature electronic failure.
Hazardous areas
- In Zone 0/1/2 or Class I Div 1/2 areas, verify the transmitter’s certification: intrinsic safety (Ex ia), flameproof (Ex d), plus ATEX, IECEx, CSA, or FM as the project requires.
- Respect entity parameters of the IS barrier when wiring intrinsically safe loops.
HART loop integrity
- HART communication requires a minimum loop resistance of approximately 250 Ω between the power supply and the HART device. Without it, the digital signal cannot ride on the analog loop reliably.
- Verify supply voltage at the transmitter terminals under load — not just at the marshalling cabinet.
6. Diagnosing Inaccurate Readings
When a temperature loop drifts or reads incorrectly, the cause is usually one of the following, in roughly this order of likelihood:
- Sensor itself — degradation, partial short, contamination of the thermowell, or insufficient immersion.
- Wiring — wrong number of leads on the RTD, broken or unshielded cable run, oxidized terminal, mismatched TC extension wire.
- Cold junction / ambient effects — transmitter exposed to direct sun, hot piping, or large ambient swings.
- Cable issues — long unshielded runs picking up EMI; impedance or grounding mismatch on the loop.
- Configuration error — wrong sensor type selected, or wrong wiring mode (2-/3-/4-wire) configured in the transmitter.
- Loop integrity — insufficient resistance for HART, unstable power, excessive cable capacitance.
Smart transmitters can flag many of these conditions automatically via HART status bits or fieldbus diagnostics. This is one of the biggest practical reasons to specify a HART model even on a loop that nominally only uses 4–20 mA.
7. Communication Protocols at a Glance
Choosing the right output protocol for a temperature transmitter is partly a function of the existing control system and partly a function of how much diagnostic and configuration access is needed.
- 4–20 mA – simplest, universally supported, no diagnostics.
- 4–20 mA + HART – the modern industrial default. Analog control signal plus a digital channel for configuration, secondary variables, and diagnostics.
- PROFIBUS PA – fully digital fieldbus, common in European process plants and Siemens-based systems. Devices share power and signal on the same pair.
- FOUNDATION Fieldbus H1 – fully digital fieldbus with distributed function blocks, common in oil & gas and large continuous-process facilities.
- WirelessHART – the same HART command set over a self-organizing 2.4 GHz wireless mesh, useful for monitoring points where cabling is uneconomic.
- Modbus RTU – widely used on packaged equipment and OEM skids.
A multi-protocol product family — for example transmitters that share hardware across HART, PA, and FF variants — significantly simplifies spares and operator training across a mixed-protocol site.
8. Applications
Smart temperature transmitters are deployed across essentially every continuous-process industry:
- Oil, gas, and petrochemical
- Power generation and district heating
- Metallurgy and steel
- Pharmaceuticals and biotechnology
- Food, beverage, and dairy
- Water and wastewater treatment
- Cement, glass, and building materials
- Pulp and paper
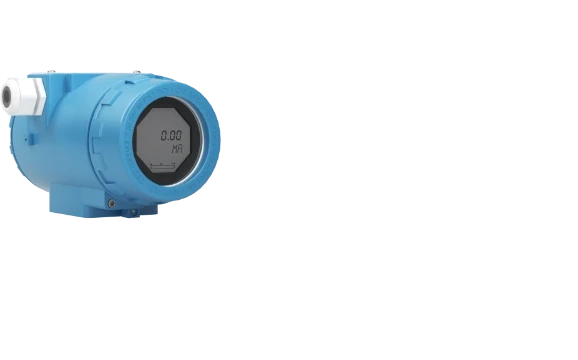
For multi-protocol plants and OEM equipment integration, Microcyber offers a complete temperature transmitter product range covering field-mount, head-mount, DIN rail, and multi-channel form factors — with HART, FOUNDATION Fieldbus, PROFIBUS PA, Modbus RTU, and 4–20 mA output options under one hardware platform:
| Series | Description | Protocols | Mounting | Product Page |
|---|---|---|---|---|
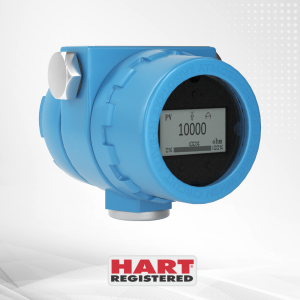
| NCS-TT105 Series | Smart Temperature Transmitter with LCD display | HART, FF, PROFIBUS PA | Field-mount | View |
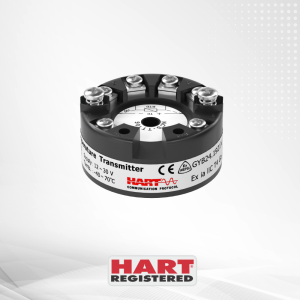
| NCS-TT106 Series | Head-mount and DIN rail variants for HART, FF, PA, Modbus RTU and 4–20 mA | HART, FF, PA, Modbus RTU, 4–20 mA | Head / DIN Rail | View |
| NCS-TT108 Series | 8-channel multi-input Smart Temperature Transmitter | FF, PROFIBUS PA | Field / DIN Rail | View |
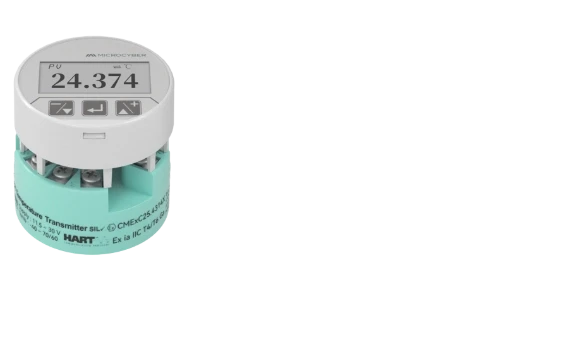
| NCS-TT306 Series | Dual-channel HART module with sensor hot backup, SIL 2 certified | HART (4–20 mA + HART) | Head / DIN Rail | View |
The NCS-TT105 / NCS-TT106 / NCS-TT108 / NCS-TT306 series share a common hardware platform and configuration toolchain, simplifying spares, training, and engineering across mixed-protocol sites.
Final Thoughts
A temperature transmitter is not just a “signal converter.” On a modern plant it is the boundary between the physical world and the digital control system, and the device that determines whether a temperature reading is trustworthy enough to control on, alarm on, or trip on.
Choosing the right protocol, installing the sensor correctly, calibrating against a traceable reference, and setting a sensible maintenance interval — those four habits separate loops that “just work” from loops that need constant attention.
If you are evaluating a temperature transmitter for a new project, the right opening questions are:
- What sensor types do I need to cover, now and in the next five years?
- What communication protocol does the control system speak?
- What hazardous-area certification does the location require?
- What accuracy and long-term stability does the application actually demand?
Answer those four questions, and most of the rest of the specification follows naturally.
Microcyber is a FieldComm Group certified Development Services Provider and PROFIBUS National Organization member, supplying smart temperature transmitters, pressure transmitters, fieldbus gateways and HART communication chips to customers in more than 40 countries. For sizing assistance, protocol selection, or OEM integration of our temperature transmitter modules, contact our application engineering team.