The “Evergreen” of Industrial Communication
Since the 1980s, the HART (Highway Addressable Remote Transducer) protocol has remained the backbone of process automation. By superimposing digital data onto traditional 4-20mA analog loops, it bridges the gap between legacy infrastructure and the modern digital factory.
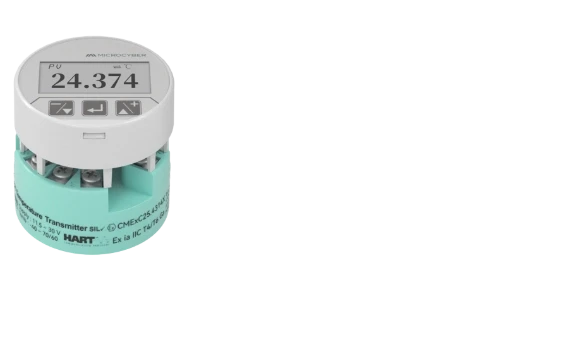
Today, with millions of HART-enabled devices installed globally—including the Microcyber NCS-TT series—this protocol is indispensable for instrumentation engineers and plant maintenance teams focused on lifecycle management.
I. Physical Layer: FSK Signaling Technology
The brilliance of HART lies in its Frequency Shift Keying (FSK) implementation, based on the Bell 202 standard.
-
Signal Superposition: HART superimposes a high-frequency digital signal on the 4-20mA current loop. This enables simultaneous transmission of analog variables and digital diagnostic data over a single pair of wires—no additional cabling required.
-
Frequency Logic: * Logic “1”: 1200 Hz
-
Logic “0”: 2200 Hz
-
-
Minimal Interference: Because the average value of the digital sine wave is zero, it causes no DC offset to the analog signal. This ensures real-time Primary Values (PV) and device status are transmitted without interruption.
Engineering Note: For high-precision loops (accuracy < 0.05%), we recommend using shielded twisted-pair cables and maintaining loop resistance between 230Ω and 1100Ω to ensure optimal FSK signal integrity.
II. Data Link Layer: Master-Slave Dynamics
HART follows a structured request-response architecture.
-
Communication Mode: A slave device (e.g., a Microcyber temperature transmitter) only responds when prompted by a master (DCS, PLC, or Handheld).
-
Dual-Master Support: The protocol allows two masters—typically a Primary Master (DCS/SCADA) and a Secondary Master (Maintenance Tool). This enables engineers to perform diagnostics without disrupting the control loop.
-
Burst Mode: For time-critical applications, Microcyber devices can be configured to “Burst Mode,” broadcasting data cyclically without waiting for master requests, achieving up to 3-4 updates per second.
III. Network Layer: Point-to-Point vs. Multi-drop
HART is adaptable to various wiring architectures:
-
Point-to-Point Mode: The most common setup. The 4-20mA signal carries the PV, while the digital signal is used for configuration and diagnostics.
-
Multi-drop Mode: Allows up to 63 devices in parallel on a single pair of wires. In this mode, the loop current is fixed at 4mA, and all data is transmitted digitally.
-
Practical Tip: To ensure power budget and response time, Microcyber engineers recommend a practical limit of 15 devices per loop.
-
IV. Application Layer: Command Hierarchy & Interoperability
To ensure seamless integration across manufacturers, HART organizes data into a tiered command set:
-
Universal Commands: Supported by all devices (e.g., Manufacturer ID, Tag, Serial Number).
-
Common Practice: Functions like range adjustment and loop calibration.
-
Device-Specific: Specialized features, such as NCS-TT sensor type selection or advanced drift diagnostics.
Integration Standards:
-
EDD (Electronic Device Description): The standard file for device parameter mapping.
-
FDI (Field Device Integration): The modern standard that unifies EDD with DTM/FDT technology for a superior software experience.
V. Technical Comparison: HART 5 vs. HART 7
For new installations, HART 7 is the industry recommendation for enhanced plant intelligence.
| Feature | HART 5 | HART 7 |
| Variables | Up to 4 | Up to 256 |
| Diagnostics | Basic | NAMUR NE 107 Compliant |
| Wireless | No | Supports WirelessHART |
| Status Monitoring | Limited | Comprehensive Device Health |
Frequently Asked Questions
-
Q: Can I use HART with existing 4-20mA wiring? A: Yes. This is HART’s biggest advantage—upgrading to “Smart” instrumentation using existing cable infrastructure.
-
Q: Why is a 250Ω resistor required? A: It converts the FSK current signal into a voltage signal that the host system can detect. Without it, communication will fail.