
Case Study: Intelligent Cooling Water System Upgrade for a Leading Fine Chemical Enterprise
A large fine chemical production enterprise in East China (annual output value >2 billion RMB) operates multiple API synthesis lines and high-temperature/pressure reaction units. The plant’s cooling water circulation system is a critical utility supporting stable reactor temperature control, distillation tower condensing, and equipment heat removal.
The original system used dozens of deep-well submersible + horizontal centrifugal pumps arranged in parallel (10+ units), controlled mainly via conventional hardwired relays and partial analog signals. With production expansion, the following issues became prominent:
- Unstable Operations: Frequent pump start/stop caused by manual intervention and aging contactors led to unstable flow/pressure, causing temperature fluctuations of ±3–5°C in key reactors.
- Monitoring Gaps: No centralized monitoring; operators needed to patrol the basement pump room frequently.
- Lack of Visibility: Piping network complex; valve status and pump performance were difficult to track in real time.
- High Costs: Energy consumption remained high due to lack of linkage control and variable frequency optimization.
- Security Concerns: Increasing cybersecurity and maintainability requirements for OT networks.

Microcyber Solution
Microcyber provided a complete fieldbus + industrial communication upgrade package:
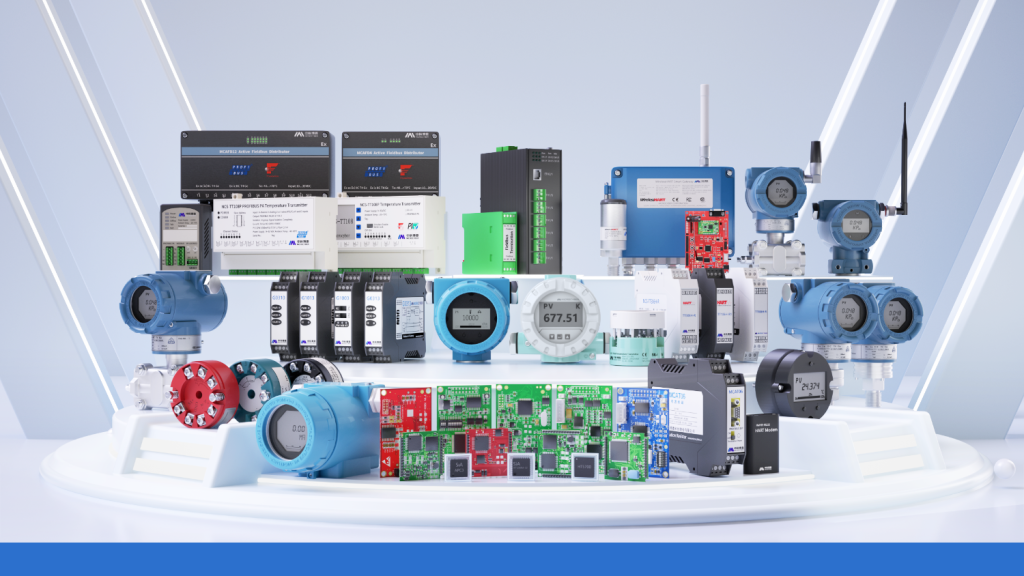
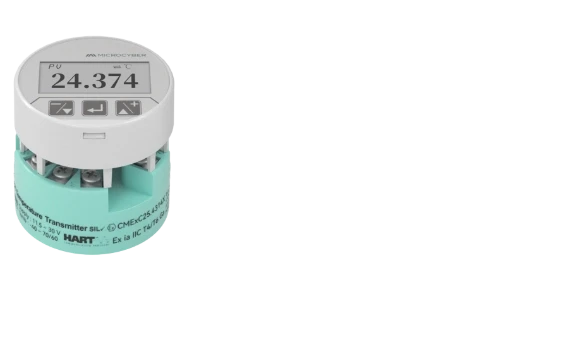
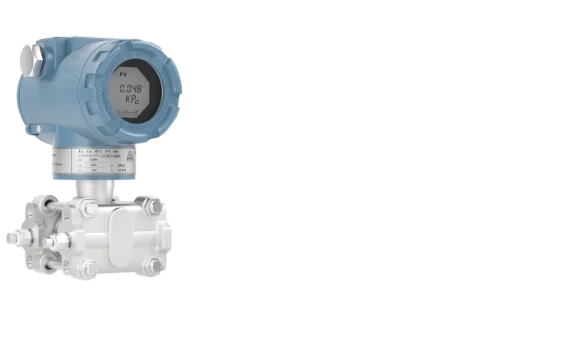
- Precision Measurement: NCS-TT106P temperature transmitters and NCS-PT105II pressure transmitters installed at key points of the main supply/return lines and chiller outlets (PROFIBUS PA protocol).
- Seamless Integration: NCS-BP105 fieldbus power conditioners and NCS-IF105P converters were used to integrate existing 4–20 mA instruments into the fieldbus segment.
- Automated Control: Pump VFDs and soft starters integrated via PROFIBUS DP, enabling group start/stop, rotation operation, and automatic standby switching.
- Predictive Maintenance: Real-time monitoring of flow, pressure, temperature, and motor vibration for proactive health tracking.

Implementation Highlights
- Hazardous Area Safety: Adopted intrinsically safe PROFIBUS PA bus in Zone 1/2, reducing wiring by ~65% compared to traditional I/O.
- Digital Accuracy: Achieved full digital communication, greatly improving signal accuracy and anti-interference capability.
- Intelligent Logic: Implemented automatic load balancing and energy-saving modes (minimum flow guarantee + VFD frequency optimization).
- Cybersecurity: Added network-level hardening measures (protocol whitelist filtering) to meet national MLPS 2.0 requirements for chemical OT environments.
Project Results
- Yield Increase: Reactor temperature control accuracy improved to ±0.8°C → product yield increased by 2.1–3.4%.
- Energy Savings: Annual electricity savings on cooling water pumps >1.2 million kWh (≈ RMB 850,000–1,000,000).
- Operational Efficiency: Reduced maintenance workload by 70%; pump failure rate dropped by 55% in the first year.
- Fast ROI: Project payback period < 14 months.
“After introducing Microcyber’s fieldbus solution, our cooling water system changed from a ‘black box’ to a transparent, manageable, and optimizable smart utility. Temperature stability directly improved product consistency, and energy savings were beyond expectation.”
— Customer Project Manager
This case demonstrates how Microcyber’s industrial communication products help chemical enterprises achieve safe, reliable, efficient, and cyber-secure utility system operation.